A supplier’s annual capacity figure is a poor answer to a buyer’s urgent question: how much saleable matcha can be released in the week when orders arrive? A line can have unused milling hours while packaging, cleaning, laboratory testing, or a late leaf delivery limits shipments. Matcha production capacity planning turns a forecast into a dated commitment at each work center. This guide gives buyers a practical way to request the figures, test the bottleneck, and agree on a capacity response before a promotion or product launch. The production scaling example is a useful starting point; the calculations below should be filled with a supplier’s measured operating data.
Contents
- What demand belongs in a matcha capacity plan?
- How do you calculate saleable kilograms per shift?
- Which production step is the true bottleneck?
- How should cleaning and changeovers enter the plan?
- What labor and skills must be available?
- How do raw materials constrain a promise?
- Where does quality release fit on the calendar?
- How much buffer should the buyer request?
- How can a buyer challenge a supplier capacity claim?
- What should the final capacity agreement contain?
1. What demand belongs in a matcha capacity plan?
Separate forecast from committed orders
Start with the customer’s required dispatch week, SKU, pack size, grade, and destination. A forecast of 1,000 kg in a month hides a sharp 700 kg first-week peak. Convert each order into the production quantity needed after expected sampling and processing loss. Use measured yield for the exact grade and format; do not copy a generic industry percentage. Then show forecast confidence and the date by which the buyer must lock artwork, packaging material, and order volume. This turns a vague annual forecast into a schedule the supplier can test.
| Demand input | Buyer supplies | Planning consequence |
|---|---|---|
| Required dispatch | Week and destination | Sets last safe release date |
| SKU mix | Grade, pack, label version | Determines changeovers |
| Firm quantity | Purchase-order kilograms | Reserves capacity |
| Upside scenario | Extra kilograms and notice | Tests surge options |
| Material approval | Artwork and component due date | Sets packaging readiness |
Ask the supplier to return two views: firm orders already loaded and available slots by week. A free slot in milling is useful only if the same lot can pass packing and release before the truck booking. If several customers share equipment, a buyer needs the capacity allocated to its SKUs, not the factory’s gross nameplate figure.
2. How do you calculate saleable kilograms per shift?
Build a transparent work-center calculation
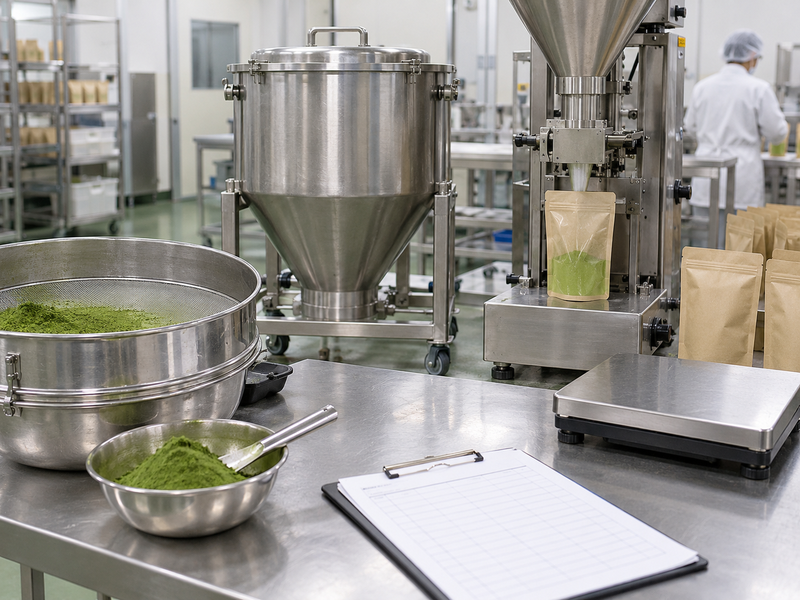
For each operation, record scheduled hours, planned breaks, expected setup and cleaning, measured running rate, and acceptable output. One useful expression is saleable kilograms per shift = productive running hours × measured kilograms per running hour × measured saleable yield. Keep the factors separate so a missed target can be traced to time, speed, or rejects. The NIST paper on overall equipment effectiveness likewise distinguishes availability, performance, and quality; it does not supply a universal matcha yield.
| Work center | Scheduled h | Lost h | Measured kg/h | Saleable yield | Saleable kg |
|---|---|---|---|---|---|
| Example milling | 8 | 1.5 | 42 | 0.96 | 262 |
| Example filling | 8 | 2 | 38 | 0.98 | 223 |
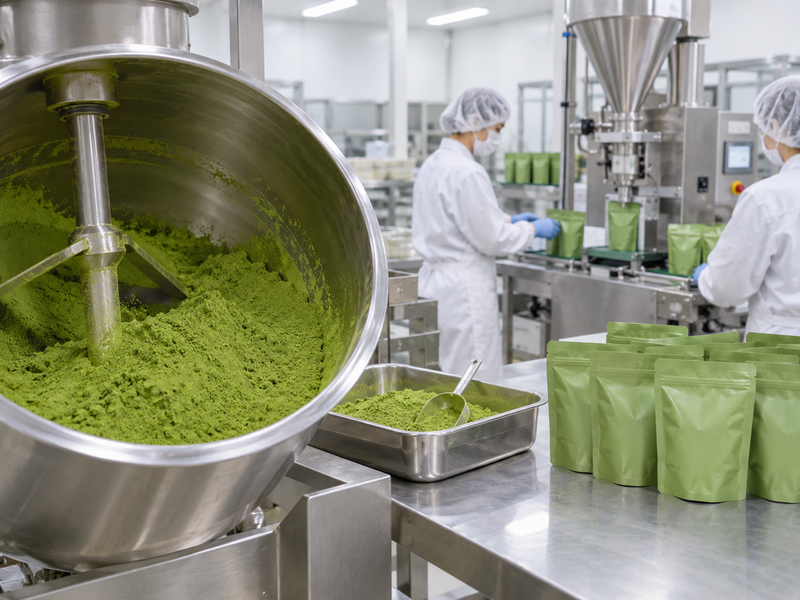
These are illustrative numbers, not a supplier benchmark. In this example, filling governs a one-shift run even though milling’s rated output is higher. Record whether the rate was demonstrated on the requested pouch, tin, or bulk bag, with the same fill weight and powder behavior. A machine acceptance test on another powder is weak evidence for a matcha shipment promise.
3. Which production step is the true bottleneck?
Follow one lot to dispatch
Map the lot through receiving, any blending or size control, filling, sealing, coding, case packing, sampling, and release. For every step, calculate the weekly saleable output using actual available shifts. The smallest feasible number on the critical route is the constraint for that SKU mix. Watch for a shared label applicator or checkweigher that appears only during packing. Also distinguish a physical bottleneck from a queue: laboratory capacity, approvals, and carrier cutoffs can limit the dispatch date without slowing the production line itself.
| Step | Weekly output possible | Shared with other SKUs? | Evidence to request |
|---|---|---|---|
| Preparation | Supplier fills in | Yes/no | Recent lot record |
| Milling or blending | Supplier fills in | Yes/no | Run-time log |
| Filling and sealing | Supplier fills in | Yes/no | Good-pack counter |
| Testing and release | Lots per week | Yes/no | Lab turnaround history |
| Dispatch | Pallets per pickup | Yes/no | Booking cutoffs |
Ask what changes when the forecast doubles. If the supplier proposes a second milling shift while filling is already saturated, the remedy does not address the constraint. NIST’s throughput case study illustrates the value of studying the actual flow and lead time rather than relying on one station’s rated speed.
4. How should cleaning and changeovers enter the plan?
Charge the schedule for SKU variety
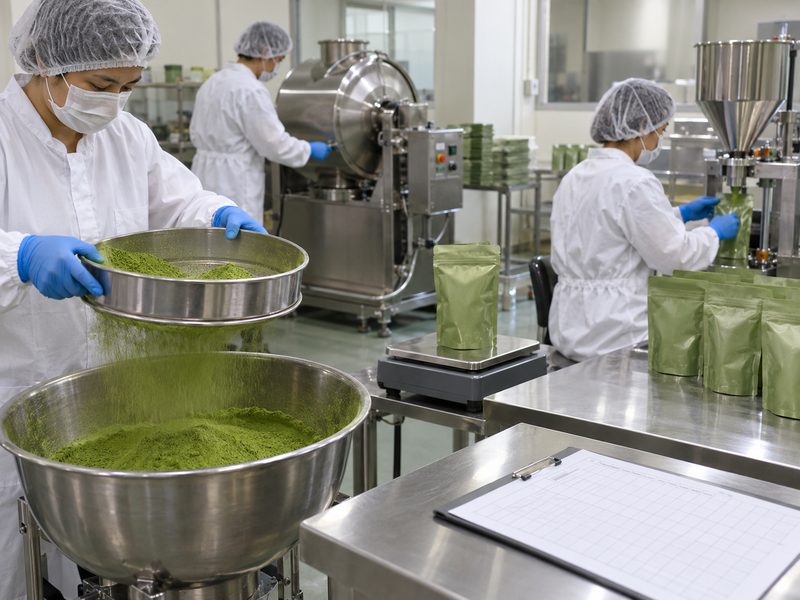
A weekly plan built from uninterrupted rated speed usually fails when orders require several grades, pack sizes, or label languages. Ask for a changeover matrix based on past runs: grade A to grade B, pouch to tin, and one artwork version to another. Include cleaning, line clearance, first-article inspection, and restart loss. The direction can matter; a change from one product family to another may require different controls than the reverse. The supplier should explain its own documented method rather than assuming one fixed setup time.
| Change | Time to reserve | Who verifies completion? | Record |
|---|---|---|---|
| Grade switch | Measured minutes | Production/quality | Clearance check |
| Pack format switch | Measured minutes | Engineering/quality | Setup approval |
| Label version switch | Measured minutes | Quality | First-article signoff |
Group similar SKUs where feasible, but check whether this creates unacceptable inventory or delays for a small order. Confirm the latest point at which the buyer can change volume or artwork without displacing another customer’s slot. A documented freeze date makes capacity discussions much more useful than a promise to be flexible.
5. What labor and skills must be available?
Count trained coverage, not headcount alone
Equipment capacity is unavailable when trained operators, maintenance support, material handlers, or quality reviewers are missing. Ask for the minimum staffing by station on each proposed shift and the cross-training plan for absences. A second shift only adds output if it has approved supervision, quality coverage, cleaning resources, and incoming material. A supplier may choose different staffing; the buyer needs the schedule to reflect its actual operating model.
| Role | Needed per shift | Backup available? | Planning check |
|---|---|---|---|
| Line operators | Supplier enters | Yes/no | Training record |
| Changeover lead | Supplier enters | Yes/no | Skill coverage |
| Quality reviewer | Supplier enters | Yes/no | Release schedule |
| Maintenance support | Supplier enters | Yes/no | Response coverage |
Where overtime or temporary staff are proposed, ask for a supervised trial at the target rate and acceptable output. Do not assume more hours produce a proportional increase in saleable kilograms. For buyers assessing a partner, the site’s quality information can frame questions about documented checks, but the specific line’s staffing and records still have to be confirmed directly.
6. How do raw materials constrain a promise?
Match supply by approved specification
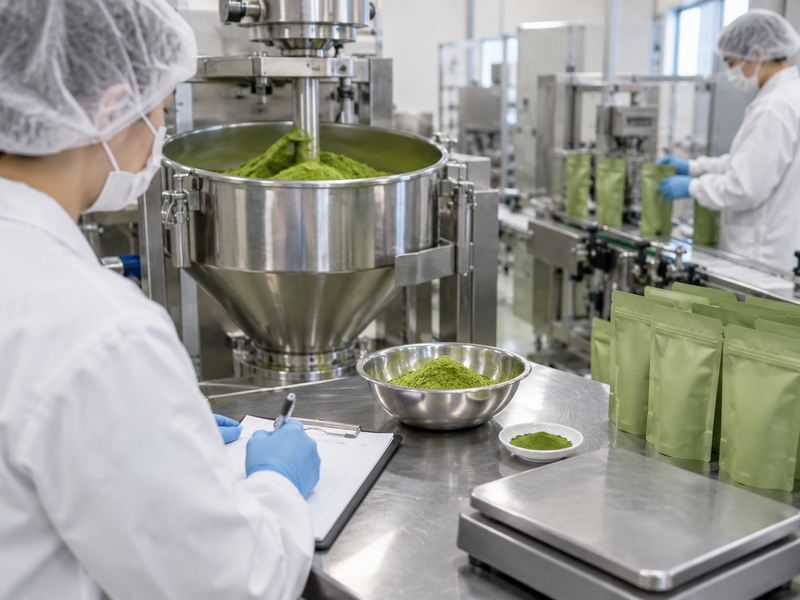
An empty production slot has little value without the approved tea material and packaging components. Request the inventory and inbound dates for the exact grade, origin or blend specification, pouch or tin, label, case, and pallet configuration. Separate physically received stock from purchase orders and stock under quality hold. If substitution is proposed, treat it as a specification and approval decision, not an automatic capacity recovery. A visual or sensory mismatch can make an on-time production run commercially unusable.
Build a simple material coverage view: starting approved stock plus confirmed receipts minus firm demand and reserved orders. Record supplier lead times and the date after which an increase cannot be supported. For scarce material, ask whether multiple approved lots can be used in one order and how traceability will be kept. The production scaling article highlights ingredient supply as a scaling factor; buyers should turn that observation into a dated, specification-specific materials plan. Packaging availability deserves the same attention because a missing printed pouch can stop a ready powder lot.
7. Where does quality release fit on the calendar?
Put a date on every hold point
Production completion and shipment readiness are different dates. Map incoming inspection, in-process checks, finished-lot sampling, required testing, document review, and release authorization. Ask whether the laboratory’s quoted turnaround starts at production finish, sample receipt, or test booking. If a result must be repeated or investigated, show how that affects the committed dispatch date. The supplier should use its approved specification and applicable market requirements; this plan does not invent a universal test panel or release limit.
| Hold point | Trigger | Owner | Typical evidence |
|---|---|---|---|
| Incoming material | Receipt | Quality | Accepted-lot status |
| First pack | Line start | Production/quality | Approved sample |
| Finished lot | Run completion | Laboratory | Results against specification |
| Shipment release | Review complete | Authorized reviewer | Signed release record |
Food manufacturing controls and records should be evaluated against the applicable rules, including 21 CFR Part 117 for covered US operations. The buyer should confirm the supplier’s actual regulatory scope and procedure. Reserve release time in the plan even when the line itself has spare hours.
8. How much buffer should the buyer request?
Tie contingency to observed variation
Do not add an arbitrary percentage to every step. Compare planned versus actual output and lead time for recent comparable lots. Note the variation caused by changeovers, maintenance, yield, test turnaround, and missed material receipts. Set a working buffer against the risks that have actually moved dispatch dates. A fast promotional launch may justify an earlier completion target; a stable recurring order may need a smaller buffer. Document who owns the cost of holding finished goods or unused material.
Use three views in the weekly review: base demand, a reasonable upside case, and a disruption case such as one lost filling shift. For each, record the earliest feasible dispatch date and the response available: another approved line, an extra staffed shift, a revised SKU sequence, or a buyer-approved split shipment. Do not list an option unless the supplier has demonstrated it for this product. A buffer is a capacity reservation with a clear trigger, not a promise that a machine will never fail.
9. How can a buyer challenge a supplier capacity claim?
Ask for a witnessed evidence pack
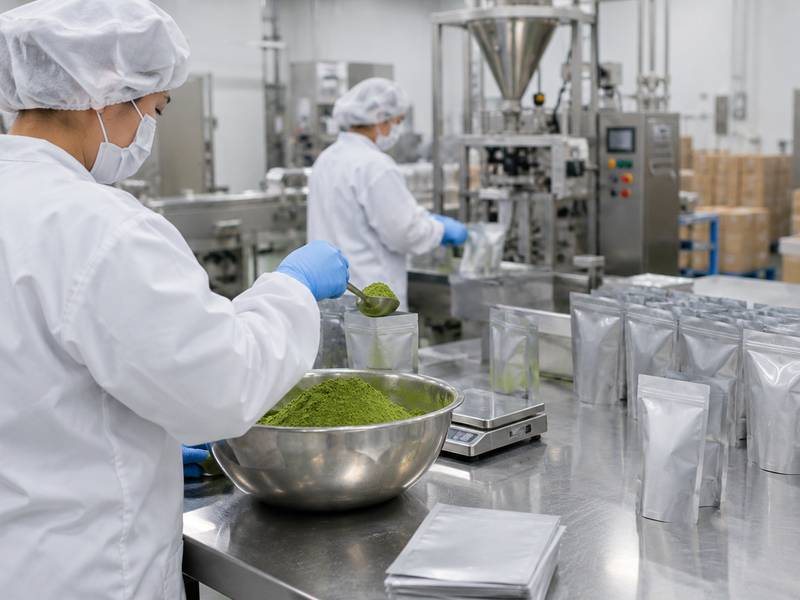
Request recent run records for a comparable matcha SKU, including scheduled time, good kilograms, rejects, setup time, and reasons for interruption. Confirm whether the figure came from a sustained shift, a short best-rate trial, or a machine brochure. Ask the supplier to repeat the calculation with the buyer’s pack size and order mix. A simple witnessed trial can reveal powder flow, seal contamination, coding, or operator handling issues before a large purchase order depends on the claimed rate.
| Supplier statement | Evidence that makes it usable |
|---|---|
| “We can make 500 kg/day” | Dated comparable shift records and good output |
| “We can add a shift” | Named staffing, QA coverage, and material plan |
| “Lead time is two weeks” | Routed schedule through testing and dispatch |
| “We have spare capacity” | Loaded schedule and allocated weekly slots |
Record the trial’s conditions and any gaps. A lower demonstrated rate is not automatically a failed supplier; it is an honest number from which the buyer can plan. The site’s bulk wholesale matcha page describes the commercial route, while the actual capacity should be agreed SKU by SKU.
10. What should the final capacity agreement contain?
Commit to quantities and decision dates
Turn the plan into a short schedule attachment to the purchase order or supply agreement. State weekly reserved saleable kilograms by SKU, the approved pack and material specification, firm-order and artwork deadlines, planned production and release windows, and the dispatch handoff. Name the owner of each input. Include a weekly review method for forecast changes, a trigger for escalation, and how both sides approve a revised promise. Commercial and legal terms should be reviewed by the parties; a spreadsheet does not replace them.
For each commitment, attach the measured assumptions: shift pattern, bottleneck rate, yield, cleaning allowance, laboratory turnaround, and material coverage. If an assumption changes, recalculate the affected week rather than quietly moving the ship date. A buyer can then see whether an increase is possible, whether a split delivery is needed, or whether the launch calendar should move. The most useful capacity plan is the one that produces a defensible answer when the next unexpected order arrives.
FAQ
Q1. Is machine nameplate capacity enough for purchase planning? No. Use measured good output on a comparable SKU and include staffing, cleaning, testing, and dispatch.
Q2. Should capacity be stated in powder or packed units? State both if needed, but commit to saleable packed units or kilograms that match the purchase order.
Q3. How often should a buyer refresh the plan? Recheck it when forecasts, SKU mix, shift coverage, or material dates change; a weekly cadence is practical for active orders.
Q4. Can a second shift solve every shortage? Only if the constrained operation, trained staff, quality coverage, and materials can support it.
Q5. What is the first document to request? Ask for a dated capacity view by work center and recent comparable run records. These reveal the gap between a headline figure and a shipment promise.